- No. 688, Jinji Road, Xiangzhou, Guangdong, China
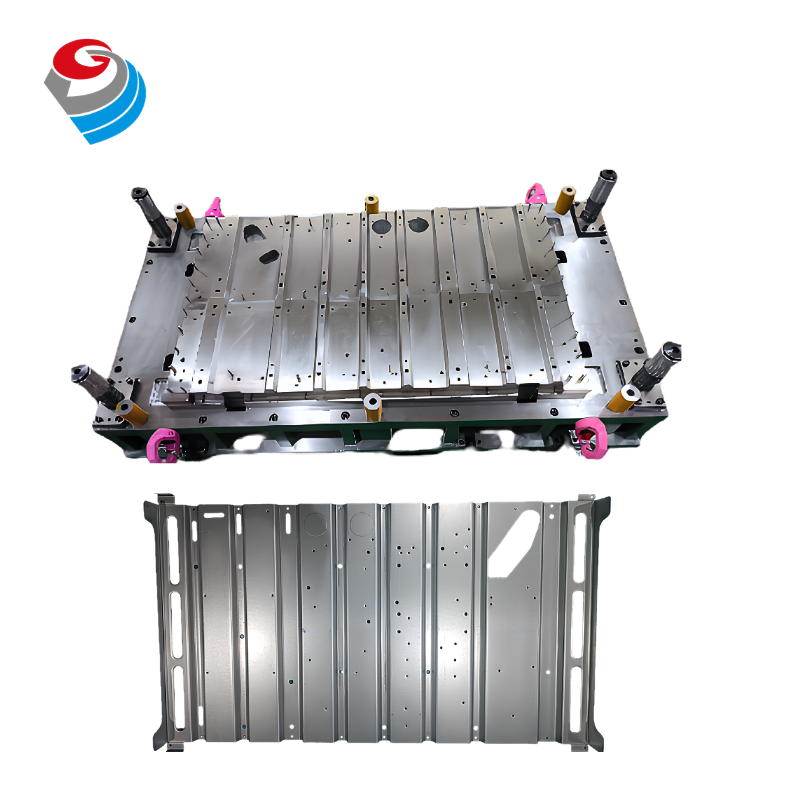
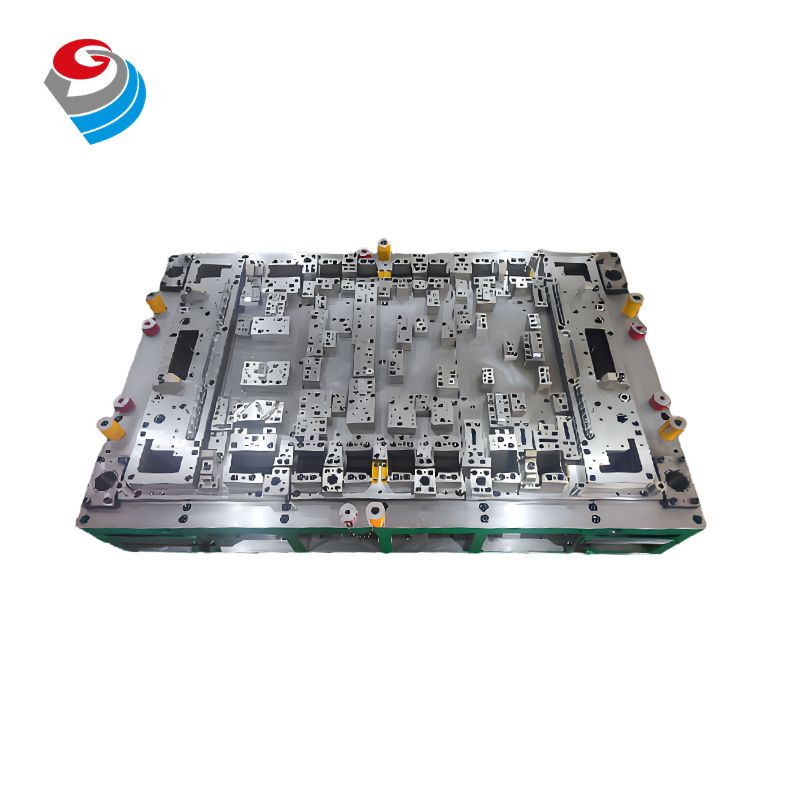
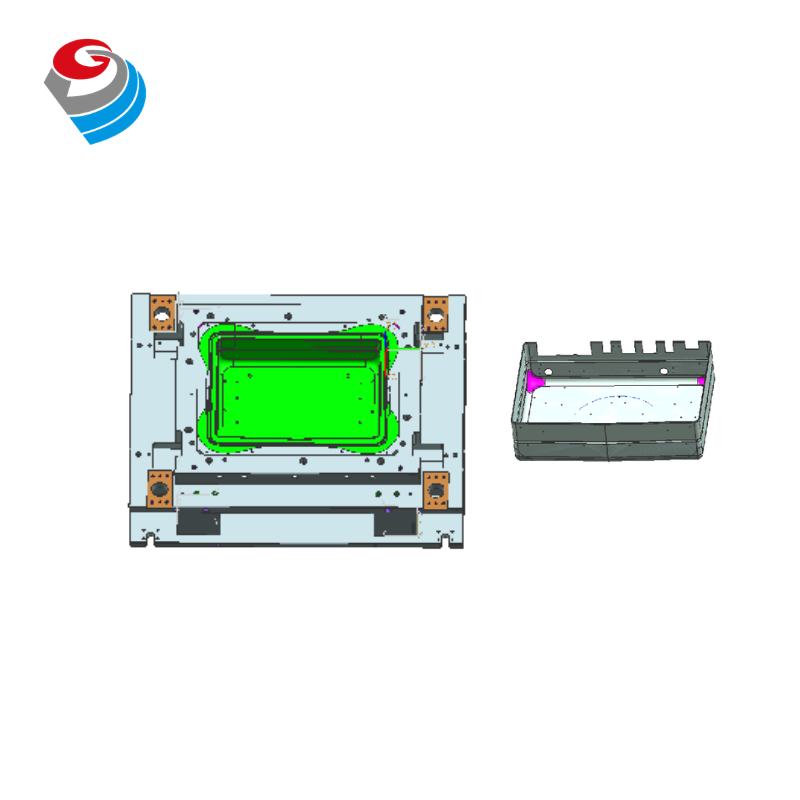
Building a stamping die for an outdoor unit base pan is a precision exercise in material matching. For this tool, we tiered the steel by function: D2, DC53, and Cr12Mo1V1 for the high-wear working inserts (punch and die cavities), P20 and 45# for the structural die holders — each grade selected for the load it actually carries. Standard parts are Misumi punches, guides, and fasteners, and the die set is built in-house, keeping every tolerance chain under one roof. The die processes SGCC, SGCD2, and DX56D deep-drawing galvanized steel at 30 strokes per minute, runs a single-out cavity, and is engineered for a 300,000-shot production life — delivered in 50–60 days
| Steel Material | P20,45#,D2,DC53,Gr12mo1v1,ect. |
| Standard Parts | Punch, Misumi, etc. |
| Die Set | Made-in-house |
| Product Material | SGCC, SGCD2, DX56D, etc. |
| Tool Cavity | 1X1 |
| Punch Speed | 30SPM |
| Delivery Time | 50-60 days |
| Tool life | 300,000 shot |
| We adopt a whole 3d modle and precision design; |
| The parts adopt a quick-switch structure; it’s convenient for workers to clean and maintain; |
| We adopt standard manufacturing; the part can suit many dies; |
| 1. Intelligent sensing mold system |
| 2. CAE algorithm predicts molding defects (accuracy > 95%) |
| 3. Reduce the secondary assembly process and increase the yield rate to 98.6% |
| 4. Adopt nano-level CNC processing + EDM micro-hole technology |
| 5. Strict quality control |
| 6. Self-lubricating microporous structure design (oil-free stamping process) |
Lorem ipsum dolor sit amet, consectetur adipiscing elit. Ut elit tellus, luctus nec ullamcorper mattis, pulvinar dapibus leo.